
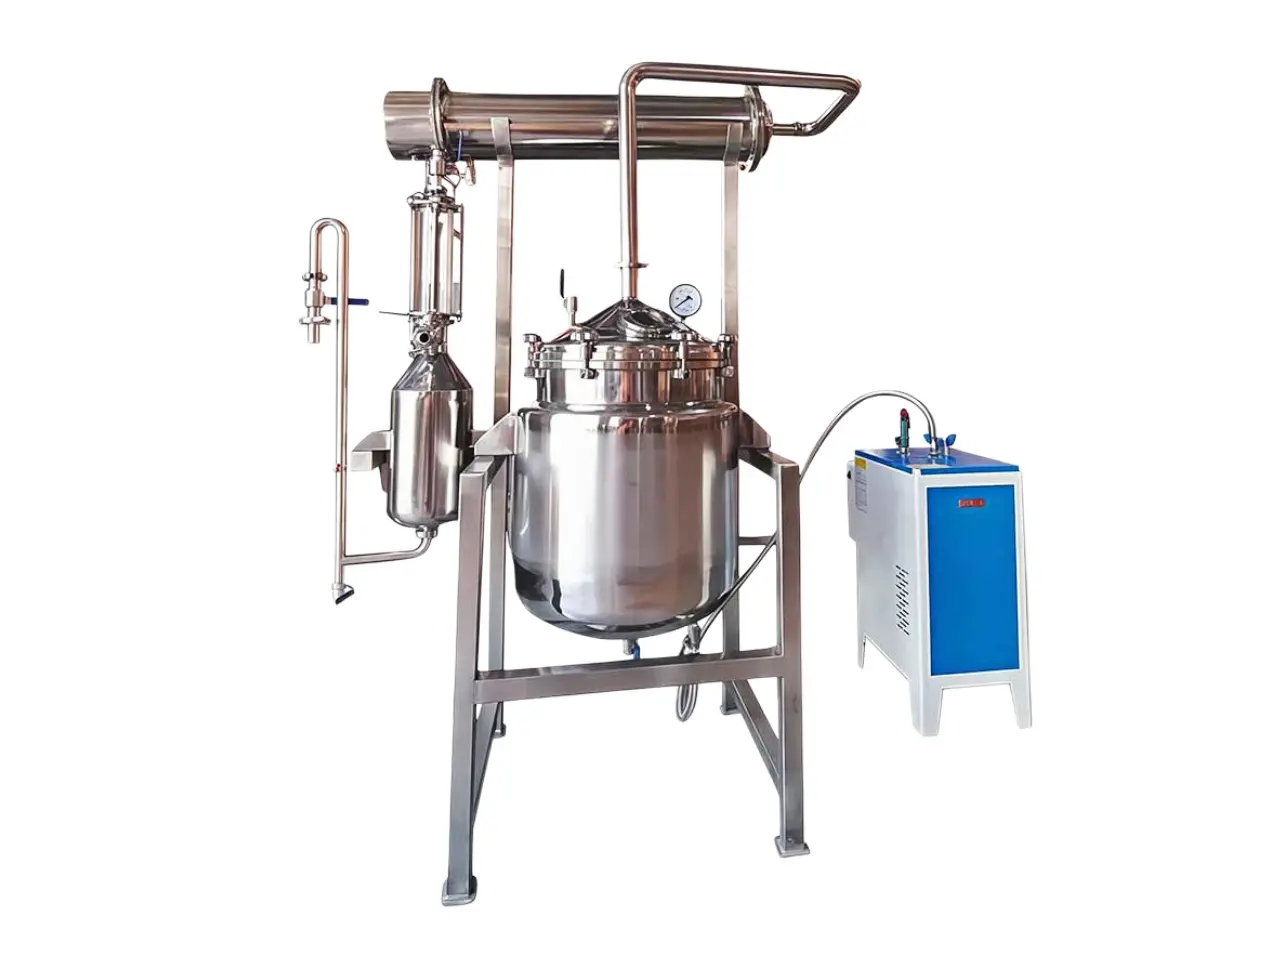
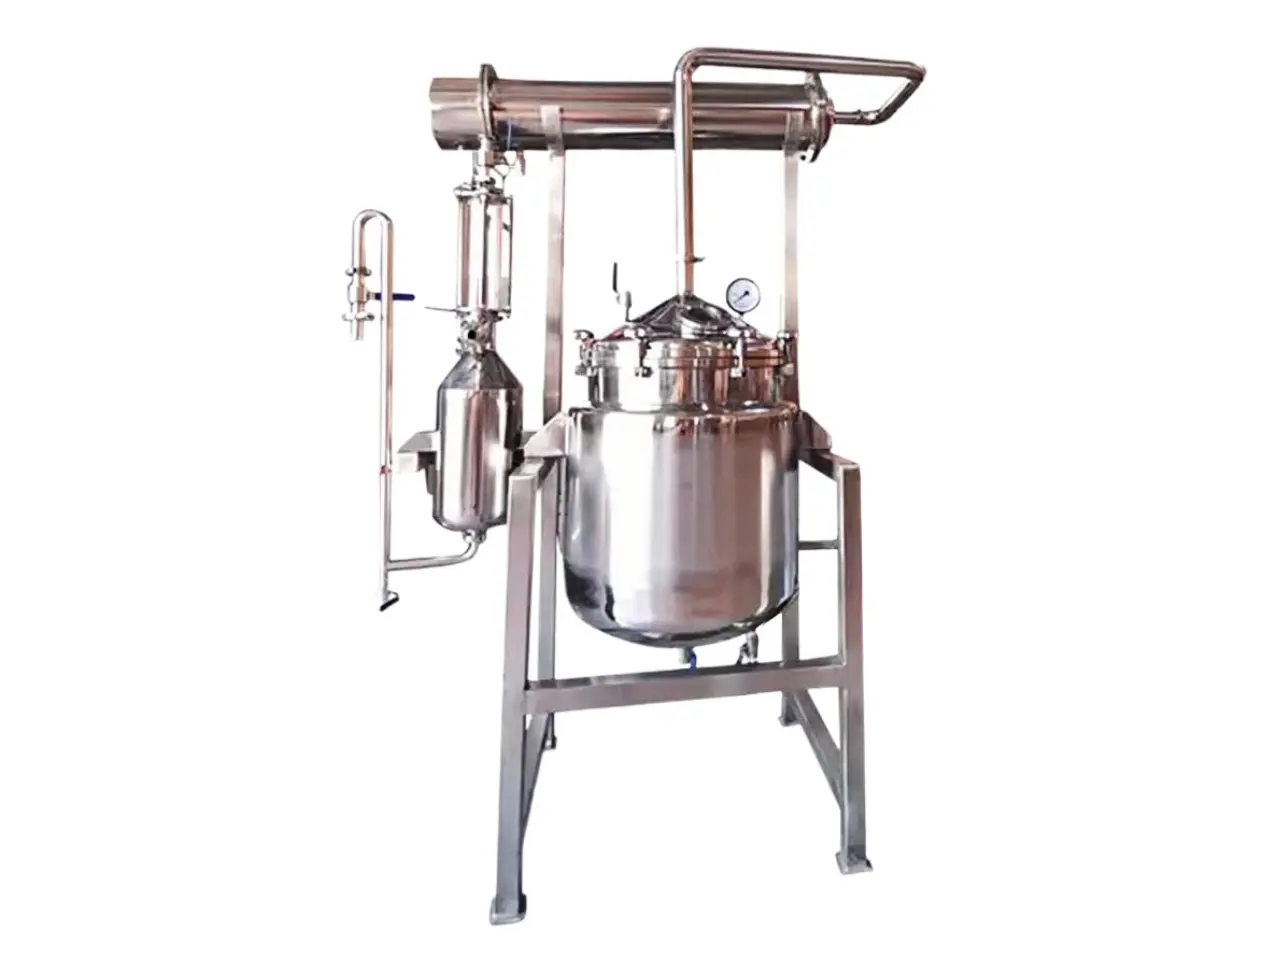
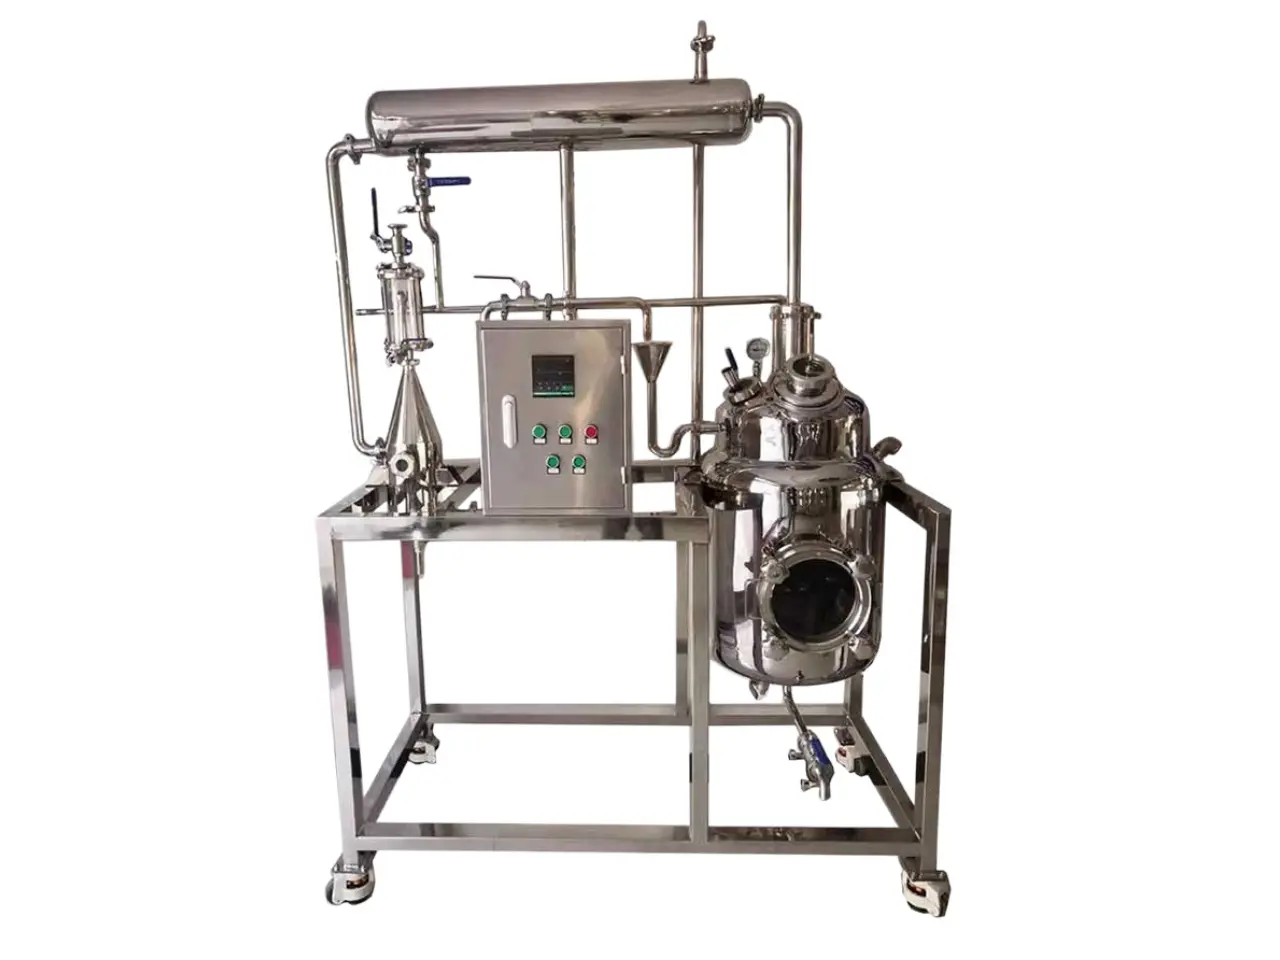
All-in-One Integrated Platform | GMP-Compliant 304/316L SS | High-Yield “Large Reflux” Technology

Steam/Water/Alcohol Extraction & Volatile Oil Recovery

Full Plug-and-Play System (Integrated Vacuum & Control)

Hygienic SUS304/316L Stainless Steel

High-Borosilicate Glass Oil-Water Separator
This Distillation Essential Oil Equipment is a fully integrated production platform specifically designed for research institutions, hospital pharmacies, and pharmaceutical enterprises for new drug development. Featuring a highly compact structural layout, it functions as premium liquid extraction equipment that performs atmospheric or negative pressure extraction, heat reflux, forced circulation, and solvent recovery within a minimal footprint. Whether for water, alcohol, or essential oil extraction equipment needs, this evaporator system offers flexible process combinations to meet high-end, small-batch, and multi-variety production requirements.
Pharmaceutical & Nutraceutical R&D: Distillation Essential Oil Equipment optimized for extracting heat-sensitive ingredients like polysaccharides and enzymes using low-temp vacuum paths.
Plant & Essential Oil Distillation: High-efficiency processing for fresh botanicals (roses, mint, etc.) with integrated organic solvent recovery.
Hospital & Customized Preparations: Perfect for small-batch, high-activity herbal pastes and proprietary medicine preparations with maximized clinical efficacy.
Industrial Pilot Testing: Simulates large-scale production line processes to provide reliable technical parameters for full-scale industrialization.
| Model Number | PC-50 | PC-100 | PC-300 | PC-500 | PC-1000 | PC-2000 |
| Extraction Tank Volume | 50L | 100L | 300L | 500L | 1000L | 2000L |
| Extraction Tank Inner Diameter | 400mm | 600mm | 700mm | 800mm | 1000mm | 1400mm |
| Extraction Tank Jacket Diameter | 500mm | 700mm | 800mm | 900mm | 1100mm | 1500mm |
| Temperature | 60-100°C | |||||
| Steam Consumption | 5kg/h | 10kg/h | 30kg/h | 50kg/h | 100kg/h | 200kg/h |
| Vacuum Pump Power | 1.1KW | 1.5KW | 2.2KW | 3KW | 4KW | 4KW |
| Electric Heating Power | 2*3KW | 2*6KW | 3*6KW | 4*6KW | 4*9KW | 4*12KW |
| Cooling Water Consumption | 500kg/h | 500kg/h | 1000kg/h | 1000kg/h | 2000kg/h | 5000kg/h |
| Extraction Time | 0.5-1h | |||||
| Heat Exchange Area | 1㎡ | 2㎡ | 6㎡ | 8㎡ | 10㎡ | 15㎡ |
| Diameter × Height | 0.5*1.5m | 0.8*1.6m | 0.9*1.8m | 1.0*1.9m | 1.2*2.5m | 1.6*3.0m |
Answer: The Heat Reflux Essential Oil Equipment utilizes a closed-loop thermal recycling system to maximize the extraction of volatile compounds. During the process, the solvent vapor is condensed and “refluxed” back into the extraction tank as a hot liquid. This continuous flow ensures that the raw material is constantly washed with fresh, heated solvent, allowing for the exhaustive removal of active ingredients. This excellent method reduces solvent consumption by up to 40% compared to traditional batch methods, ensuring a successful and highly concentrated final yield.
Answer: By integrating vacuum technology into the Distillation Essential Oil Equipment, the internal pressure is lowered, which effectively reduces the boiling point of both water and the essential oils. This allows distillation to occur at much lower temperatures, typically between 50°C and 65°C. This is perfect for protecting heat-sensitive terpenes and delicate aromatic molecules that would otherwise be destroyed by high heat. This elite thermal management ensures the biological activity and fragrance profile of your oils remain absolutely intact.
Answer: The Distillation Essential Oil Equipment is equipped with a high-efficiency shell-and-tube condenser and a specialized oil-water separator. As the vaporized steam and oils enter the cooling zone, they are rapidly liquified. Because essential oils have a different specific gravity than water, the separator allows for the precise and effortless collection of the pure oil layer. This extraordinary recovery rate is ideal for pharmaceutical-grade production where maintaining the integrity of the chemical profile is an ultimate requirement for the final product.
Answer: We manufacture the contact surfaces of this Distillation & Heat Reflux Essential Oil Equipment from high-grade 316L stainless steel to provide superior resistance to chemical corrosion. Many essential oils contain acidic or reactive components that can cause pitting in standard metals over time. 316L contains molybdenum, which offers a sturdy and reliable layer of protection against stress-corrosion cracking. This construction ensures a long service life and meets the most rigorous GMP and food-grade sanitary standards for global export.
Answer: To achieve a professional and repeatable production cycle, the Heat Reflux Essential Oil Equipment is integrated with a digital control panel that monitors vacuum levels, jacket temperatures, and flow rates in real-time. By utilizing a Variable Frequency Drive (VFD), operators can fine-tune the heating and agitation intensity to match the specific density of the botanical material. This level of technical oversight allows you to master the extraction parameters, ensuring that every batch meets the exact same quality specifications. This consistency is successfully achieved through pioneering engineering.
“Still have questions? Contact our technical team for a free consultation.”
We will contact you within one working day. Please pay attention to your email.
Automatic Vacuum Honey Processing & Filtering Machine
Vacuum Low-Temperature Liquid Extraction & Concentration Unit
Custom Steam Distillation & Heat Reflux Essential Oil Equipment
WhatsApp: +8615736768129
Email: [email protected]
Address: Zhengzhou, Henan Province, China


COPYRIGHT© 2026 Zhengzhou Panchi Machinery Equipment Co., Ltd. | Privacy Policy

Our team will respond within 24 hours.
Thanks! We'll get back to you within 24 hours.
Check your inbox (and spam folder) for our reply.