
Pharmaceutical manufacturing requires extremely precise control over every stage of production. Whether producing active pharmaceutical ingredients (APIs), intermediates, or specialized formulations, manufacturers must maintain consistent reaction conditions to achieve reliable product quality.
However, traditional reaction systems often face challenges such as uneven mixing, unstable temperature control, solvent handling difficulties, and limited process flexibility.
A modern pharmaceutical vacuum reactor provides a controlled environment that helps manufacturers overcome these challenges by combining vacuum technology, efficient agitation, and accurate temperature management.
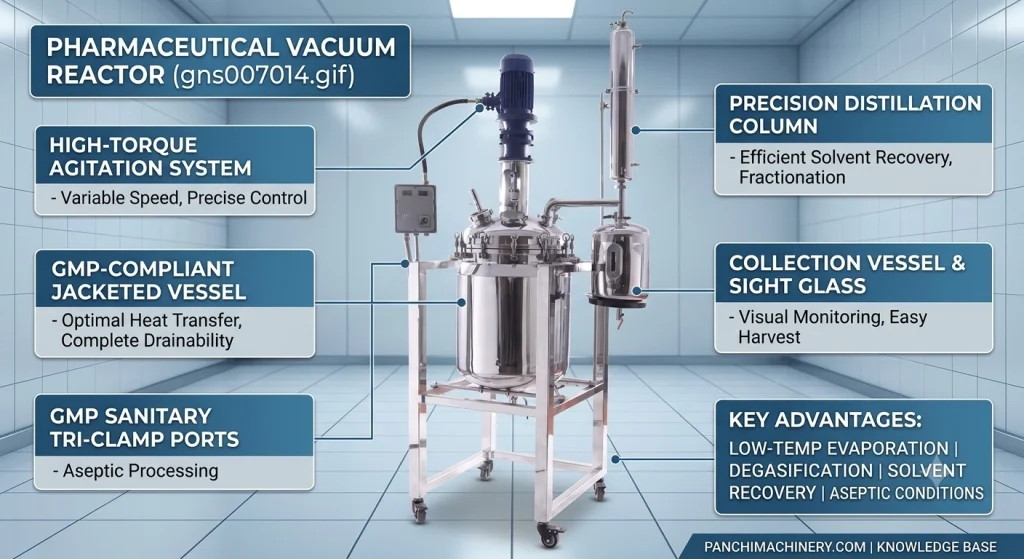
Unlike conventional atmospheric reactors, vacuum reactors operate under reduced pressure conditions. This allows manufacturers to process heat-sensitive pharmaceutical materials at lower temperatures while improving evaporation, reaction efficiency, and product protection.
For pharmaceutical companies, selecting the right reactor system is not only about vessel capacity. It also involves evaluating:
These factors directly influence production efficiency, product consistency, and compliance with pharmaceutical manufacturing standards.
A pharmaceutical vacuum reactor is a specialized processing vessel designed for pharmaceutical reactions under controlled vacuum conditions.
It integrates several functions, including:
The main difference between a vacuum reactor and a standard atmospheric reactor is the operating pressure inside the vessel.
By creating a vacuum environment, the system can reduce the boiling point of liquids and improve the removal of solvents or moisture at lower temperatures.
This is especially valuable for pharmaceutical applications where excessive heat may damage sensitive compounds.
A typical pharmaceutical vacuum reactor system includes:
The equipment configuration can be customized according to:
For pharmaceutical manufacturers, a properly designed reactor provides better process control and helps maintain consistent production quality.
Vacuum technology plays an important role in pharmaceutical processing because many pharmaceutical materials are sensitive to temperature, oxidation, and moisture.
A controlled vacuum environment provides several process advantages.
Under vacuum conditions, liquids can evaporate at lower temperatures compared with atmospheric pressure.
This helps manufacturers:
For applications involving valuable pharmaceutical compounds, maintaining a stable low-temperature environment can significantly affect product performance.
Many pharmaceutical reactions involve solvents that must be removed after processing.
A vacuum environment improves solvent evaporation efficiency while reducing the required processing temperature.
This can help manufacturers achieve:
Some pharmaceutical materials may react with oxygen during processing.
Vacuum operation reduces oxygen exposure inside the reactor, helping protect sensitive compounds and improve process stability.
Mixing is one of the most critical functions of a pharmaceutical reactor.
A pharmaceutical process often requires precise distribution of:
Poor mixing can lead to:
A well-designed pharmaceutical vacuum reactor uses an appropriate agitation system to achieve uniform mixing throughout the vessel.
The agitator design depends on factors such as:
For example, low-viscosity liquids may require high-speed mixing, while high-viscosity pharmaceutical materials may need stronger torque and specialized impeller designs.
By combining vacuum operation with optimized mixing performance, manufacturers can create more stable and efficient reaction conditions.
The performance of a pharmaceutical reaction depends not only on the reactor vessel itself but also on how effectively the system controls mixing, reaction conditions, and heat transfer.
In pharmaceutical production, even small variations in processing conditions can affect:
A well-designed pharmaceutical vacuum reactor combines mechanical agitation, precise temperature control, and vacuum regulation to create a stable processing environment.
These functions work together to improve reaction performance and support reliable pharmaceutical manufacturing.
Mixing is one of the most important functions of pharmaceutical reactor equipment.
During pharmaceutical production, different materials must be evenly distributed throughout the vessel. This includes:
Insufficient mixing may cause:
Therefore, the agitator design must match the specific characteristics of the processed materials.
Different pharmaceutical applications require different mixing solutions.
Common agitator designs include:
Paddle agitators are suitable for gentle mixing applications where maintaining product structure is important.
They are commonly used for:
Anchor agitators are often selected for high-viscosity pharmaceutical materials.
Their large contact area helps:
This makes them suitable for products requiring consistent temperature distribution.
Some pharmaceutical formulations require stronger mixing forces.
High-shear systems can improve:
The correct agitation solution depends on:
A customized pharmaceutical reactor equipment configuration helps manufacturers achieve better process results.
A major advantage of a vacuum reactor system is the ability to control reaction conditions more precisely.
Vacuum operation can influence:
For pharmaceutical applications, controlling these factors helps manufacturers maintain repeatable production results.
Many pharmaceutical reactions involve organic solvents that require careful handling.
A vacuum environment helps lower evaporation temperatures, allowing manufacturers to remove solvents more efficiently.
Benefits include:
This is especially useful for reactions involving temperature-sensitive compounds.
Some pharmaceutical ingredients degrade when exposed to:
Vacuum processing helps create a gentler reaction environment.
By reducing oxidation risk and controlling evaporation conditions, manufacturers can improve product stability.
Accurate temperature control is essential for pharmaceutical reactions.
A reaction that runs too hot or too cold may result in:
A modern pharmaceutical vacuum reactor usually integrates a jacketed heating and cooling system.
The jacket surrounding the reactor vessel allows heat transfer between the process material and the external heating or cooling medium.
Common options include:
This design provides more uniform temperature distribution compared with direct heating methods.
Pharmaceutical production requires accurate monitoring of operating parameters.
Important control factors include:
Automation systems can help operators maintain consistent conditions during each batch.
For GMP-oriented manufacturing, advanced monitoring and control improve process reliability and documentation.
Material selection is another key factor when choosing a pharmaceutical reactor vessel.
Most pharmaceutical applications require stainless steel construction due to:
Common materials include:
For stricter pharmaceutical applications, a GMP reactor vessel may require additional design considerations, including:
These features help reduce contamination risks and support pharmaceutical production standards.
A properly configured vacuum reactor system provides manufacturers with better control over mixing, reaction conditions, and temperature management. The next section will explore the major applications of pharmaceutical vacuum reactors, including API synthesis, solvent processing, emulsification, and other industrial pharmaceutical processes.
A pharmaceutical vacuum reactor is used in a wide range of pharmaceutical production processes where precise reaction control, uniform mixing, and stable temperature management are required.
Compared with conventional reaction vessels, vacuum reactor systems provide greater flexibility for handling sensitive materials, reducing solvent content, and improving process consistency.
The actual application depends on:
For pharmaceutical manufacturers, selecting the right reactor configuration helps improve production efficiency while maintaining product quality.
One of the most important applications of a pharmaceutical vacuum reactor is active pharmaceutical ingredient (API) synthesis.
During API manufacturing, chemical reactions often require strict control of:
A vacuum environment provides additional control by allowing manufacturers to process materials under reduced pressure.
This can improve:
For complex pharmaceutical reactions, uniform mixing is especially important because uneven material distribution may result in incomplete reactions or inconsistent product properties.
A properly designed reactor with suitable agitation ensures that reactants are evenly dispersed throughout the vessel.
Many pharmaceutical production processes involve solvents that must be removed after reaction or extraction.
A vacuum reactor system can improve solvent removal by reducing the boiling temperature of liquids.
This provides several advantages:
This is particularly useful when processing heat-sensitive pharmaceutical compounds.
Compared with atmospheric evaporation, vacuum operation allows manufacturers to remove solvents under milder conditions while maintaining product stability.
In some production lines, the reactor can be integrated with:
This creates a more efficient and controlled processing workflow.
Pharmaceutical formulations often require precise mixing of multiple components.
Examples include:
In these applications, the reactor must provide:
A customized agitation system helps achieve the required mixing performance.
Depending on the formulation, manufacturers may select:
For high-viscosity pharmaceutical materials, anchor-type designs can improve circulation and reduce material buildup on vessel walls.
For formulations requiring particle dispersion or emulsion formation, high-shear mixing systems may provide better results.
Pharmaceutical manufacturing requires strict control of contamination risks.
A GMP reactor vessel should be designed to support hygienic processing and easy cleaning.
Important design features include:
Stainless steel is widely used because it provides:
For demanding pharmaceutical applications, SUS316L stainless steel is often selected because of its higher resistance to chemical corrosion.
A well-designed stainless steel reactor tank supports cleaner production conditions and helps manufacturers meet strict quality requirements.
Selecting suitable equipment requires evaluating both production requirements and process conditions.
The reactor size should match:
Choosing the correct capacity helps avoid unnecessary investment while ensuring sufficient production flexibility.
Different pharmaceutical processes may involve:
The reactor material must provide adequate chemical resistance.
Common options include:
The mixing system should match the characteristics of the materials.
Consider:
Incorrect agitator selection may lead to poor mixing performance and longer processing cycles.
Modern pharmaceutical production increasingly requires accurate monitoring and repeatable operation.
A complete pharmaceutical reactor equipment solution may include:
These features help improve production consistency and reduce operator workload.
| Selection Factor | Why It Matters |
|---|---|
| Reactor Material | Determines corrosion resistance and sanitation |
| Vacuum Capability | Supports low-temperature processing |
| Agitation Design | Ensures uniform mixing |
| Temperature Control | Maintains stable reaction conditions |
| Automation Level | Improves repeatability and efficiency |
A carefully selected reactor system allows pharmaceutical manufacturers to achieve better process control and more reliable production outcomes.
The next section will introduce PCM’s customized pharmaceutical vacuum reactor solutions and explain how manufacturers can configure reactor systems based on their specific production needs.
Choosing the right reactor system is a critical decision for pharmaceutical manufacturers because equipment performance directly affects product quality, production efficiency, and process reliability.
PCM provides customized pharmaceutical vacuum reactor solutions designed for different pharmaceutical, chemical, and laboratory production requirements. Instead of using a standard configuration for every application, PCM engineers the reactor system according to:
A customized reactor solution helps manufacturers achieve more stable operation and better control throughout the production process.
PCM pharmaceutical reactor systems can be configured with different options to meet specific manufacturing needs.
Pharmaceutical applications require equipment that can withstand chemical exposure while maintaining hygienic performance.
PCM reactors can be manufactured with:
These materials provide:
For strict pharmaceutical applications, a properly designed stainless steel reactor tank helps support cleaner and safer processing conditions.
Different pharmaceutical materials require different mixing and heating solutions.
PCM reactor systems can be equipped with customized:
These configurations help manufacturers achieve:
By combining precise agitation with vacuum operation, a vacuum reactor system provides better control for complex pharmaceutical processes.
Pharmaceutical production requires strict attention to hygiene and contamination prevention.
A properly designed GMP reactor vessel should consider:
PCM focuses on practical engineering details to help manufacturers build reliable and maintainable pharmaceutical production systems.
A high-performance pharmaceutical vacuum reactor is more than a reaction vessel. It is a complete processing solution that combines:
For pharmaceutical manufacturers, selecting the right equipment configuration can improve production consistency, reduce processing risks, and support long-term manufacturing goals.
PCM provides customized reactor solutions for applications including:
Contact PCM to discuss your pharmaceutical reactor requirements and receive an engineered solution based on your production process.
A: A pharmaceutical vacuum reactor is used for controlled pharmaceutical reactions, mixing, solvent removal, and temperature-sensitive processing. It helps manufacturers improve reaction stability and product consistency.
A: Vacuum technology reduces the boiling point of liquids, allowing manufacturers to process materials at lower temperatures. This helps protect sensitive compounds and improve solvent removal efficiency.
A: Pharmaceutical reactors are commonly manufactured from stainless steel, especially SUS304 and SUS316L. These materials provide corrosion resistance, durability, and hygienic performance.
A: Selection depends on production capacity, material characteristics, mixing requirements, temperature control needs, and sanitary standards. A customized pharmaceutical reactor equipment solution ensures better process performance.


Whatsapp: +8615736768129
Email: [email protected]
Address: Zhengzhou, Henan Province, China
Automatic Vacuum Honey Processing & Filtering Machine
Vacuum Low-Temperature Liquid Extraction & Concentration Unit
Custom Steam Distillation & Heat Reflux Essential Oil Equipment
SS304/316L Low-Temperature Vacuum Scraper Concentrator
QN Spherical Vacuum Concentrator & Alcohol Recovery Unit
Multi-function Stainless Steel Vacuum Distillation & Extraction Unit
Hot Reflux Vacuum Liquid Extraction & Concentration Unit
Single-Effect External Circulation Vacuum Concentrator
SJN Series Double-Effect External Circulation Vacuum Evaporator
We will contact you within one working day. Please pay attention to your email.
Automatic Vacuum Honey Processing & Filtering Machine
Vacuum Low-Temperature Liquid Extraction & Concentration Unit
Custom Steam Distillation & Heat Reflux Essential Oil Equipment
WhatsApp: +8615736768129
Email: [email protected]
Address: Zhengzhou, Henan Province, China


COPYRIGHT© 2026 Zhengzhou Panchi Machinery Equipment Co., Ltd. | Privacy Policy

Our team will respond within 24 hours.
Thanks! We'll get back to you within 24 hours.
Check your inbox (and spam folder) for our reply.