
In industrial botanical processing, biopharmaceutical isolation, and crude herb formulation facilities, deploying an engineered vacuum concentration process determines whether a facility maintains molecular integrity or suffers catastrophic active yield loss. When standard open-kettle evaporation vessels run under ambient atmospheric pressure, they introduce severe thermal toxicity. When raw liquid extracts are subjected to standard processing thresholds approaching 100 degrees Celsius, crucial thermolabile phytochemicals—including volatile alkaloids, delicate glycosides, and complex polysaccharides—suffer rapid thermal cracking and severe irreversible denaturing. For plant managers looking to evaluate standard mechanical parameters and baseline system configurations, these physical hardware footprints are fully detailed in our separate equipment sizing manual Herbal Concentration Unit Case Study.
In contrast, mastering the underlying physics of the vacuum concentration process requires analyzing the localized molecular residence times and high fluid-film velocities along the heat-exchange boundary layer. To optimize liquid-film vaporization homogeneity within the subsequent heating tubes and eliminate sudden pressure drops caused by macro-particulates, routing the dense raw botanical slurry through a sanitary Stainless Steel Colloid Mill prior to the concentration loop provides radical wet-method particle size reduction. Shearing complex suspended plant fibers to completely smooth out subsequent boiling gradients prevents micro-explosions and bubble flashing at the heat exchanger wall. Beyond immediate component degradation, legacy atmospheric boiling methods introduce crippling mechanical bottlenecks:
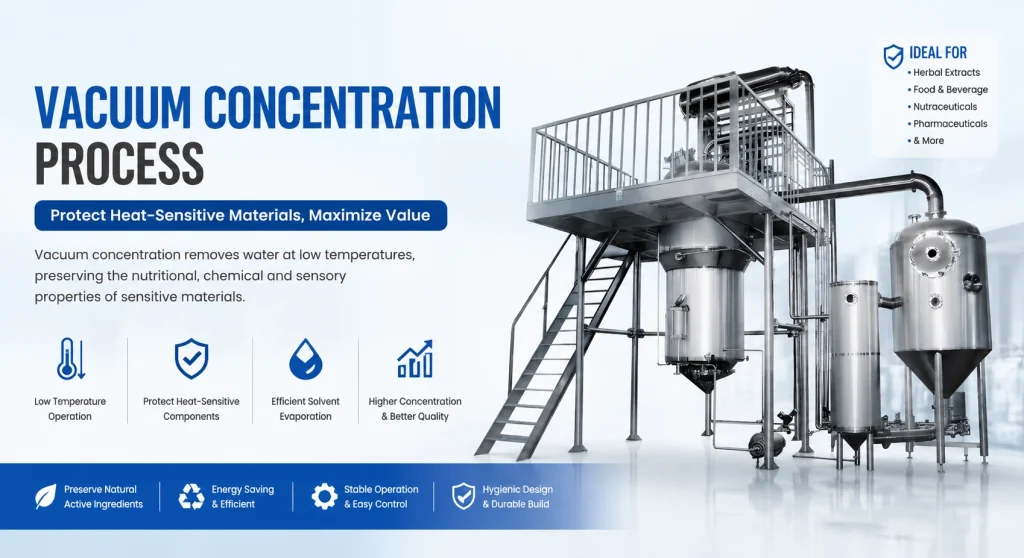
By shifting the operational envelope toward a continuous, low-temperature vacuum concentration process, facilities alter the absolute vapor-liquid equilibrium (VLE). This thermodynamic adjustment ensures that phase changes occur under suppressed conditions, completely avoiding the critical activation energy required for thermal hydrolysis, oxidative browning, and ring-opening degradation pathways.
Achieving a repeatable concentration endpoint while preventing active constituent loss requires strict alignment along the localized vapor-liquid equilibrium (VLE) curve. Panchi Machinery avoids standard static pan designs; instead, our engineering utilizes balanced mechanical negative pressure suppression coupled with optimized multi-pass product recirculation currents. By operating a dedicated vacuum concentration process, processing plants can stabilize their thermodynamic cycles and protect product purity.
By maintaining a continuous internal process vacuum of -0.086 MPa to -0.094 MPa across our specialized product line, the boiling threshold of water-based extracts drops from 100 degrees Celsius down to an optimal window of 42 to 52 degrees Celsius. This low-temperature operating envelope ensures the structural integrity of heat-sensitive bio-actives.
In multi-ton botanical processing setups, routing raw liquid extracts directly into an industrial Double Effect External Circulation Vacuum Evaporator as the primary flash desolventization phase allows operations to strip away 90% of the initial solvent volume at high velocities without fouling tube walls. Implementing a specialized Double Effect Vacuum Evaporator layout allows the thermodynamic cycle to leverage an advanced energy cascade: high-temperature live steam heats the first-effect calandria, vaporizing the initial solvent phase under vacuum. This generated secondary vapor is then directed into the shell side of the second-effect evaporator body to act as its driving thermal source.
By utilizing a Double Effect Vacuum Evaporator, the system minimizes live steam demand by approximately 50 percent compared to single-effect hardware. Inside the vertical tubes of the heat exchanger, the herbal fluid enters an optimized external circulation loop driven by intense natural density differentials or forced axial flow. This stage of the vacuum concentration process forms an ultra-thin, high-velocity film along the electropolished tube walls, maximizing the overall heat transfer coefficient (U-value) while preventing product stagnation and localized burning.
Procurement committees and site engineering teams must cross-examine true mechanical specifications over generic equipment descriptions to guarantee predictable product performance during scale-up. Selecting a proper vacuum concentration process framework requires breaking down each distinct extraction and concentration engineering design.
The Hot Reflux Vacuum Liquid Extraction & Concentration Unit represents an elegant architectural coupling of volatile extraction and downstream concentration inside a single, hermetically sealed operational loop. When deploying Hot Reflux Extraction methodologies, liquid solvents are heated within the extraction calandria, and the rising solvent vapors are directed straight into a high-capacity overhead condensation array. The cooled, distilled solvent is then returned to the extraction chamber, bathing the raw botanical bed in a continuous counter-current fluid path.
This layout establishes a highly dynamic Hot Reflux Extraction gradient that accelerates mass transfer out of the plant cell wall. Because the solvent is concentrated inline while simultaneously re-priming the primary extraction bed, raw fluid volume demands drop by 50 to 60 percent compared to basic decoupled extraction tanks. Utilizing this custom machine to run your vacuum concentration process ensures that variable frequency dosing pumps and an automated liquid level tracking loop prevent drying out or boiling spikes across long-duration continuous operations.
Specifically engineered to combat the degradation of extremely thermolabile botanical molecules, the Vacuum Low-Temperature Liquid Extraction & Concentration Unit implements a deep-set vacuum baseline that consistently operates down to -0.097 MPa. This system relies heavily on automated Vacuum Liquid Extraction loops to suppress the boiling point of aqueous solutions down to 35 to 40 degrees Celsius, creating an incredibly gentle processing environment that protects sensitive vitamins, essential enzymes, and highly volatile flavor monoterpenes.
Advanced Vacuum Liquid Extraction mechanics feature an expanded cross-sectional diameter with thin-wall electropolished SUS316L processing tubes. As the fluid Brix escalates above 35% and natural thermal siphoning degrades, the system must transition downstream into a specialized Low Temperature Vacuum Scraper Concentrator. The integrated Teflon wipers mechanically scour the electropolished wall, disrupting the stagnant boundary layer and preventing high-density botanical syrups from baking or caramelizing during the final formulation steps of the vacuum concentration process.
The Multi-Function Stainless Steel Vacuum Distillation Extraction Unit is designed as a flexible, versatile non-standard processing platform engineered for pilot plants and multi-product processing facilities. This system integrates Multi-Function Stainless Steel Extraction paths, allowing operators to alternate between water-based steam distillation, alcohol-based cold maceration, negative pressure vacuum separation, and high-purity solvent rectification within a single physical footprint.
Facilities using Multi-Function Stainless Steel Extraction platforms benefit from a heavy-duty fractional column packed with structured SUS316L corrugated wire mesh internals, maximizing vapor-liquid contact stages to yield solvent recovery purities up to 95% Vol. This versatility optimizes the global vacuum concentration process, while an advanced multi-port valve manifold allows the process lines to switch flow configurations instantly, avoiding product stagnation and accommodating diverse raw materials ranging from delicate floral leaves to dense botanical roots.
For heavy industrial processing demanding bulk water or solvent stripping, the SJN Series Double Effect External Circulation Vacuum Evaporator is the benchmark for thermal efficiency. This specific Double Effect Vacuum Evaporator utilizes a two-stage thermal cascade where the first effect operates at a moderate vacuum (-0.04 MPa) and higher temperature, while the second effect runs at a deep vacuum (-0.09 MPa) and low temperature. The secondary vapor generated from the raw material in the first effect is channeled directly into the heating calandria of the second effect, acting as its sole driving heat source.
This configuration cuts live steam usage by up to 50% compared to traditional single-stage designs. Furthermore, its external circulation layout uses high natural density siphoning to drive fluid velocities through the vertical tubes at speeds exceeding 1.5 m/s. This high turbulent velocity generates a self-scouring action along the electropolished tube walls, drastically reducing boundary layer fouling and allowing the system to easily handle high-density botanical extracts up to 40 Brix.
| Sizing & Material Benchmarks | Hot Reflux Extraction & Concentration Unit | Low-Temperature Liquid Concentration Unit | Multi-Function Stainless Steel Extraction Unit | Double Effect External Circulation Evaporator |
| Primary Process Function | Continuous loop solvent extraction with direct inline concentration. | Process-optimized handling of highly thermolabile molecules. | Versatile pilot and batch-scale multiphasic product separation. | High-throughput bulk volume solvent stripping and concentration. |
| Material Specification | Contact Focus: SUS316L / Outer Trim: SUS304 | Contact Focus: SUS316L / Outer Trim: SUS304 | Contact Focus: SUS316L / Outer Trim: SUS304 | Contact Focus: SUS316L / Outer Trim: SUS304 |
| Internal Surface Finish | Ra <= 0.4 micron (Electropolished) | Ra <= 0.38 micron (Mirror-Grade Finish) | Ra <= 0.4 micron (Electropolished) | Ra <= 0.45 micron (Sanitary Satin Polish) |
| Normal Process Vacuum Hold | -0.085 MPa to -0.092 MPa | -0.092 MPa to -0.097 MPa | -0.085 MPa to -0.095 MPa | -0.080 MPa to -0.094 MPa |
| Live Steam Consumption | ~0.6 kg per kg of water evaporated. | ~0.65 kg per kg of water evaporated. | ~0.62 kg per kg of water evaporated. | ~0.32 kg per kg of water evaporated (Energy Saving). |
| Typical Target Brix Limits | 15 – 45 Brix concentration range. | 10 – 40 Brix concentration range. | 10 – 50 Brix flexible range. | 10 – 30 Brix intermediate range. |
| Automation Specification | Siemens HMI Panel / PID Logic loops. | Full SCADA data logging / S7-1500 PLC architecture. | Modular digital control stack with remote logging. | Central DCS interface ready for distributed plant tracking. |
Reviewing how advanced fluid loops function over basic boiling kettles identifies why generic commercial options suffer from inconsistent batch results and frequent sanitation challenges. When evaluating an industrial vacuum concentration process, legacy market alternatives prioritize low material cost, while Panchi Machinery focuses on strict ASME BPE compliance and optimized fluid velocities.
| Process Metric | Traditional Atmospheric Evaporation | Advanced Vacuum Concentration Process |
| Boiling Thermal Threshold | Constant 100°C (Water) / 78°C (Ethanol). | Controlled 35°C – 52°C under deep negative loops. |
| Boundary Layer Velocity | Stagnant, near-zero fluid movement. | > 1.5 m/s via forced axial/thermosiphon currents. |
| Latent Heat Utilization | Vented to atmosphere (Single pass loss). | Re-routed as driving steam in secondary effects. |
| Foam & Entrainment Control | Manual anti-foam agents / High carryover loss. | Centrifugal mist separators with automatic PLC ballasts. |
Below is the verified mechanical general arrangement layout of Panchi Machinery’s industrial-scale external circulation distillation, concentration, and mass-transfer array:
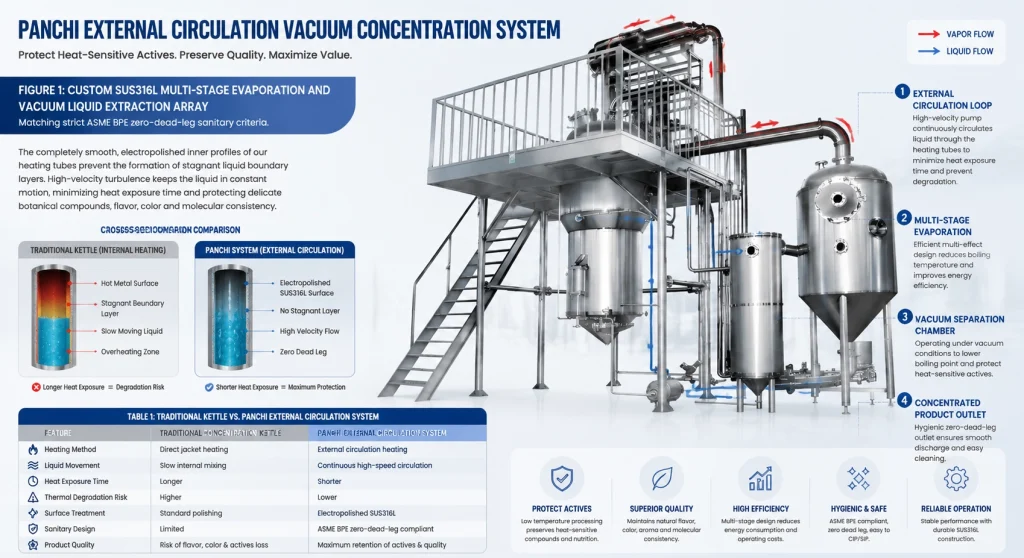
Figure 1: Custom SUS316L Multi-Stage Evaporation and Vacuum Liquid Extraction array matching strict ASME BPE zero-dead-leg sanitary criteria.
The completely smooth, electropolished inner profiles of our heating tubes prevent the formation of stagnant liquid boundary layers. In standard concentration kettles, these slow-moving boundary layers remain in contact with hot metal surfaces for too long. This continuous overheating breaks down active botanical components and ruins the flavor, color, and molecular consistency of the final herbal concentrate.
To demonstrate how a regulated vacuum concentration process insulates highly thermolabile botanical structures, we examine the molecular preservation profile of complex glycoside matrices during solvent removal. While specific plant footprint dimensions, batch weights, and raw processing volumes are fully tabulated in our downstream hardware log Herbal Concentration Unit Case Study, the focus here belongs to fluid-film degradation kinetics.
When processing complex botanical juices, high thermal exposure breaks down fragile glycoside chains through unintended thermal hydrolysis. By maintaining a continuous negative pressure gradient, the system restricts the maximum localized fluid temperature. High-performance liquid chromatography (HPLC) validation profiles confirm that minimizing thermal residence times limits the activation energy available for oxidative browning. The resulting concentrated extract matches international monograph purity benchmarks, ensuring that high-density intermediates retain their original bio-active molecular distributions without structural caramelization.
Operating advanced thermal evaporation trains and large Double Effect Vacuum Evaporators overseas requires precise on-site preparation and structured engineering validation. Panchi Machinery coordinates a comprehensive onboarding framework to ensure safe utility deployment and strict compliance with global factory safety codes.
Before our engineering dispatch team arrives at the client’s facility for mechanical integration, the plant must provision and route these specific service links directly to our hookup boundaries to guarantee the stability of the vacuum concentration process:
Once the final mass-transfer target is reached, the hyper-concentrated botanical intermediate must be vacuum-discharged straight into an ASME BPE-compliant Vertical Stainless Steel Storage Tank. Equipped with 360-degree orbital CIP spray balls and electropolished to a mirror finish (Ra ≤ 0.4 μm), this collection vector isolates the finished concentrate from atmospheric bio-burden. For pharmaceutical installations matching cGMP standards, Panchi provides full traceability documentation.
Installation Qualification (IQ) protocols cover raw material certifications (MTRs confirming SUS316L heat trace bounds) and certified weld logging with borescope validation. Operational Qualification (OQ) executes loop testing of all automated pneumatic valves, alarms, and PID loop stability under simulated water runs. Finally, Performance Qualification (PQ) maps batch consistency, solid Brix drift, and active compound mass balances across three consecutive true-material validation batches.
To maintain high heat transfer rates and protect critical vacuum seals from premature failure, plant maintenance staff must follow a structured service schedule for the entire machinery stack executing the vacuum concentration process:
Q: What causes product foaming inside the vacuum separation chamber, and how is it stopped?
A: Product foaming is typically caused by sudden vacuum drops, high boiling rates, or saponin fractions within the herbal matrix. When raw extract enters a high-vacuum zone too quickly, dissolved air flashes instantly, creating a thick foam blanket that can carry over into the condenser. To stop this, the control system must use a proportional vacuum modulation valve to smoothly ramp up the negative pressure profile. Panchi Machinery also includes a mechanical foam-breaking impact plate at the chamber inlet, paired with automated anti-foaming fluid injection points managed directly by the central PLC.
Q: How does the external circulation system handle high-viscosity concentrations without plugging the tubes?
A: The system prevents tube plugging by combining high-efficiency thermal siphoning with optional forced axial circulation pumps. As the liquid extract concentrates and rises in viscosity, natural thermal siphoning slows down. The control system monitors this change via inline pressure drop sensors. If fluid velocity drops below 1.2 m/s, the PLC engages the variable-frequency forced circulation pump. This input increases fluid turbulence along the tube walls, preventing boundary layer stagnation and ensuring an efficient vacuum concentration process even at high Brix targets.
Q: Can this concentration unit process solvent-extracted materials safely?
A: Yes. When processing ethanol or solvent-heavy herbal extracts, the unit running your vacuum concentration process can be configured with full explosion-proof protection. All localized electrical systems—including pump drives, pneumatic control boxes, and level instruments—carry certified ATEX Zone 1 or Class I, Division 1 / Group D explosion-proof ratings. The system also utilizes pure PTFE-enveloped gaskets and dual mechanical shaft seals with pressurized barriers to completely eliminate solvent leakage into the production facility.
Our application engineering division is fully equipped to deliver a 1-to-1 non-standard process simulation for your specific site conditions, encompassing precise vacuum load calculations, condensing surface calculations, and complete material traceability logs (MTRs). Please submit your daily throughput requirements and raw material characteristics below. Our team will provide a comprehensive technical proposal—complete with CAD general arrangement drawings—and an official commercial quotation within 24 hours.


Whatsapp: +8615736768129
Email: [email protected]
Address: Zhengzhou, Henan Province, China
Automatic Vacuum Honey Processing & Filtering Machine
Vacuum Low-Temperature Liquid Extraction & Concentration Unit
Custom Steam Distillation & Heat Reflux Essential Oil Equipment
SS304/316L Low-Temperature Vacuum Scraper Concentrator
QN Spherical Vacuum Concentrator & Alcohol Recovery Unit
Multi-function Stainless Steel Vacuum Distillation & Extraction Unit
Hot Reflux Vacuum Liquid Extraction & Concentration Unit
Single-Effect External Circulation Vacuum Concentrator
SJN Series Double-Effect External Circulation Vacuum Evaporator
We will contact you within one working day. Please pay attention to your email.
Automatic Vacuum Honey Processing & Filtering Machine
Vacuum Low-Temperature Liquid Extraction & Concentration Unit
Custom Steam Distillation & Heat Reflux Essential Oil Equipment
WhatsApp: +8615736768129
Email: [email protected]
Address: Zhengzhou, Henan Province, China


COPYRIGHT© 2026 Zhengzhou Panchi Machinery Equipment Co., Ltd. | Privacy Policy

Our team will respond within 24 hours.
Thanks! We'll get back to you within 24 hours.
Check your inbox (and spam folder) for our reply.